Explore our CE-compliant, high-clarity water-soluble essences and active botanical compounds engineered for maximal bioavailability.




Analysis of Solubilization Dynamics, Molecular Bioavailability, and Global Market Shifts in Botanical Processing.
The global phytopharmaceutical and functional botanical market is undergoing a structural transition. Legacy crude plant extracts, characterized by low lipophilic absorption, high turbidity in liquid matrices, and rapid sedimentation, are being rapidly phased out by Tier-1 product formulation engineers. Modern consumer demand across North America, Europe, and Asia-Pacific heavily favors ready-to-drink (RTD) functional beverages, effervescent nutraceutical supplements, transparent cosmetic serums, and bio-compatible oral tinctures.
Achieving immediate, crystal-clear liquid dissolution without compromising the physiological activity of key phytochemicals (such as polysaccharides, ginsenosides, hypericin, polyphenols, and avenanthramides) represents the central technical barrier for brand owners. As a specialized CE Certified Water-Soluble Herbal Essence Supplier, Shenzhen Rubrum Biologics Co., Ltd. resolves this industrial challenge through proprietary micro-encapsulation, spray-drying atomization, and ultrasonic-assisted micellar dispersion technology.
Traditional botanical extraction relies heavily on organic solvent reflux (ethanol, methanol, ethyl acetate). While effective for raw compound separation, solvent residues often compromise EU Novel Food regulations and cause precipitation when introduced into water-based client formulations.
| Parameters | Standard Crude Extracts | Conventional Hydro-Alcoholic Extracts | Rubrum CE Water-Soluble Herbal Essence |
|---|---|---|---|
| Cold Water Dissolution | Poor (< 20%), leaves high residue | Moderate (30%-50%), cloudy haze | Instant (99.9%), 100% transparent |
| Particle Size Distribution | 50 - 250 Microns (μm) | 10 - 50 Microns (μm) | < 100 Nanometers (nm) |
| Turbidity (NTU Rating) | > 45.0 NTU (Highly Opaque) | 15.0 - 30.0 NTU (Cloudy) | < 0.5 NTU (Crystal Clear) |
| Thermal Stability (80°C Beverage Pasteurization) | Precipitates & degrades active markers | Partial thermal degradation | Thermostable active compound retention |
| Heavy Metal & Residue Limit | Variable (Requires strict re-testing) | Solvent Trace Risk (> 50 ppm) | CE & EU Regulation (EC) 396/2005 Compliant |
Navigating International Quality Frameworks: CE Mark, cGMP, EU Novel Food, and FDA GRAS Benchmarks.
European buyers enforce stringent toxicological standards. Our CE-certified production lines strictly adhere to EU Regulation (EU) 2015/2283 for novel food ingredients, ensuring residual pesticide levels meet Regulation (EC) 396/2005 and PAH4 contamination remains below actionable thresholds.
For US and Canadian B2B clients, ingredient consistency is non-negotiable under 21 CFR Part 111 (cGMP for Dietary Supplements). Every production lot of Shenzhen Rubrum Biologics includes full Analytical Certificates (CoA) validated by third-party ISO 17025 accredited laboratories.
From raw wild-harvested St. John’s Wort to certified organic Hericium Erinaceus fruiting bodies, our GAP (Good Agricultural Practices) certified farms implement full batch-to-farm barcode traceability to guarantee zero adulteration.
Unlocking Unrivaled Production Cost Efficiency, Rapid Customization, and High Capacity Automated Extraction.
China remains the epicenter of global botanical cultivation and secondary active-ingredient extraction. Shenzhen Rubrum Biologics Co., Ltd. leverages this ecosystem to deliver institutional-grade herbal extracts at globally competitive cost structures. By positioning advanced manufacturing hubs close to core botanical agricultural zones in Shaanxi, Jilin, and Yunnan, we secure direct access to fresh, uncompromised raw plant materials.
Enabling Versatile Product Formulations Across Functional Foods, Cosmeceuticals, and Pharmaceutical Formulations.
In liquid beverage formulations, typical botanical powders cause unwanted sediment rings, turbidity, and gritty mouthfeel. Our water-soluble essences dissolve instantly in cold liquids, yielding completely transparent energy shots, relaxing herbal teas, and electrolyte enhancement drinks.
Botanical actives like Oat Avenanthramides and Grapefruit Naringin require maximum dermal bio-penetration. Water-soluble nano-emulsions allow seamlessly stable integration into high-end cosmetic serums, anti-redness lotions, and hydrogel facial masks without oil phase separation.
Modern consumers favor pectin and gelatin gummies over traditional hard capsules. Water-soluble Lion's Mane and Reishi extracts ensure uniform molecular dispersion throughout the gummy base during thermal setting, guaranteeing consistent dosage per serving.
Pioneering Research, Enterprise Quality Control, and Worldwide Botanical Ingredient Supply Chain Leadership.
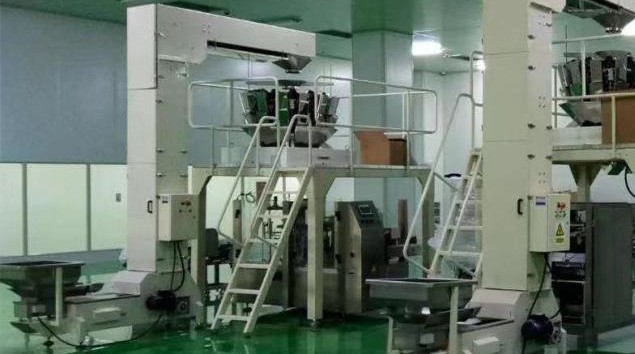
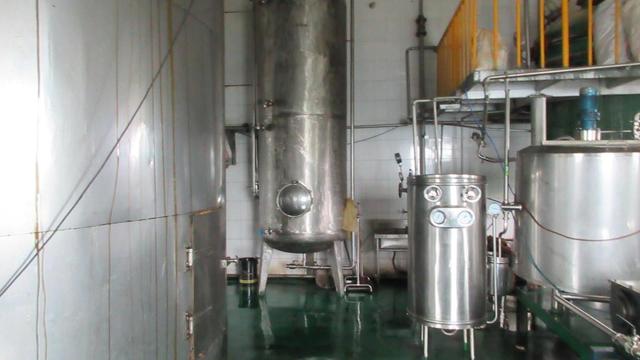
Shenzhen Rubrum Biologics Co., Ltd. is a leading China herbal extract manufacturer specializing in the research, development, production, and supply of high-quality natural plant extract ingredients for the food, supplement, and cosmetic industries. With a strong focus on innovation, quality assurance, and sustainable sourcing, the company serves customers worldwide with reliable botanical ingredient solutions.
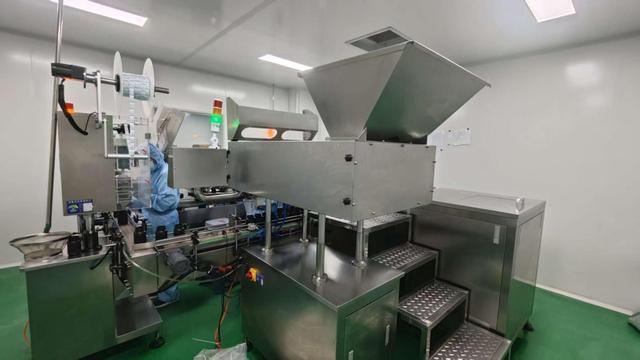
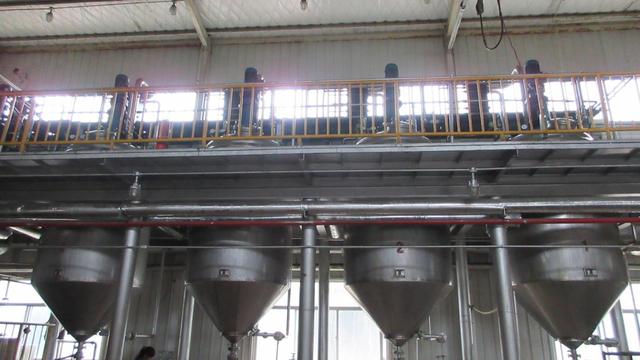
Leveraging advanced extraction technologies and modern manufacturing facilities, Shenzhen Rubrum Biologics offers a comprehensive portfolio of herbal extracts, botanical powders, natural active ingredients, and customized plant-based formulations. Its products are widely used in dietary supplements, functional foods, beverages, nutraceuticals, personal care products, cosmetics, and wellness applications.
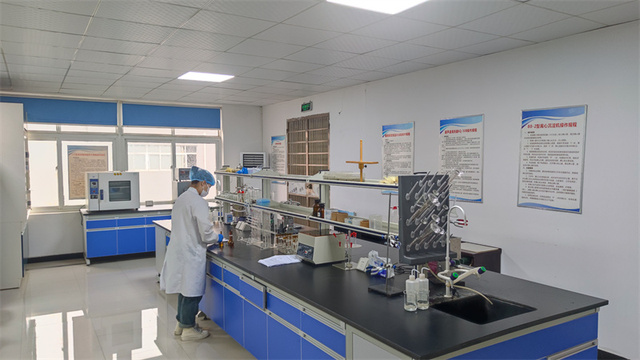
The company is committed to maintaining the highest standards throughout the entire production process, from raw material selection to final product delivery. By implementing rigorous quality control procedures and advanced analytical testing methods, Shenzhen Rubrum Biologics ensures product consistency, purity, and safety in accordance with international quality requirements.
Driven by a dedicated research and development team, the company continuously explores innovative extraction technologies and new botanical applications to meet the evolving needs of global markets. Customized solutions are available to help customers optimize product performance, enhance formulation efficiency, and accelerate product development.
With a customer-oriented philosophy, competitive manufacturing capabilities, and a stable global supply network, Shenzhen Rubrum Biologics Co., Ltd. has established long-term partnerships with manufacturers, distributors, and brand owners across numerous countries. The company remains committed to delivering premium natural plant extract ingredients that support healthier lifestyles and sustainable industry development worldwide.
Clear Answers to Common Questions Regarding Water Solubility, Custom OEM Blending, and Shipping Compliance.
Complete water solubility requires eliminating water-insoluble plant cell wall fibers, hydrophobic lipids, and heavy waxes. Shenzhen Rubrum Biologics employs targeted enzymatic breakdown, high-pressure homogenization, and micro-encapsulation techniques that encapsulate hydrophobic active molecules within hydrophilic carrier systems, preventing aggregation or cloudiness even after extended shelf storage.
CE marking and rigorous European safety standard compliance indicate that our manufacturing protocols meet stringent European health, safety, and environmental protection standards. This eliminates customs delays, streamlines regulatory filings for end-products, and assures global buyers of zero heavy metal contamination and pesticide residue compliance.
Yes. We offer fully customized extraction ratios (such as 10:1, 20:1, 50:1) as well as exact chemical marker quantification (e.g., St. John's Wort standardized to 0.3% Hypericin, Echinacea standardized to 7% Polyphenols by HPLC). Every custom batch includes a detailed analytical Certificate of Analysis (CoA).
Because highly refined water-soluble powders naturally possess hydrophilic properties, they should be stored in original sealed double-layer polyethylene inner bags, housed inside moisture-proof fiber drums. Store in a cool, dry warehouse below 25°C and under 60% relative humidity.
Our standard trial batch MOQ starts at 1kg for high-purity standardized compounds and 25kg (standard drum size) for commercial manufacturing production runs. Complimentary sample evaluation kits (10g–50g) are available upon request for qualified corporate product development labs.
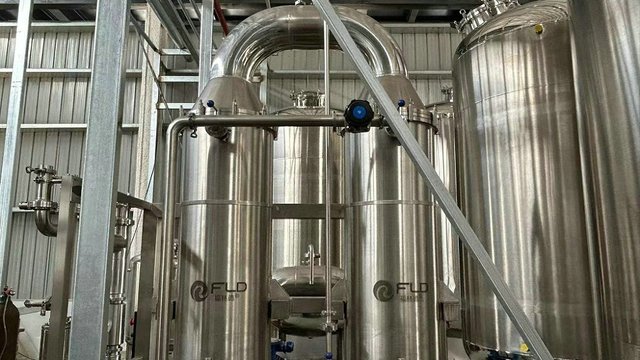
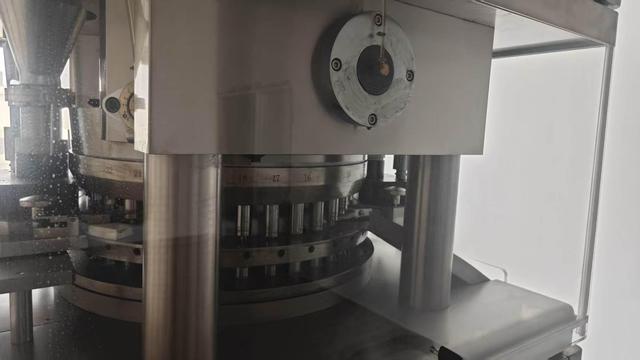
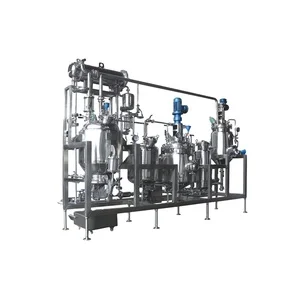
Beyond supplying raw ingredients, Shenzhen Rubrum Biologics provides turnkey private-label solutions including custom multi-herb premixes, tableting, capsule filling, and industrial extraction equipment (such as our 50L–500L multifunctional ultrasonic extraction units).
Discover additional high-purity botanical actives, medicinal mushroom extracts, and extraction machinery solutions.





 Rubrum Biologics